Products >> Railway Brake >>
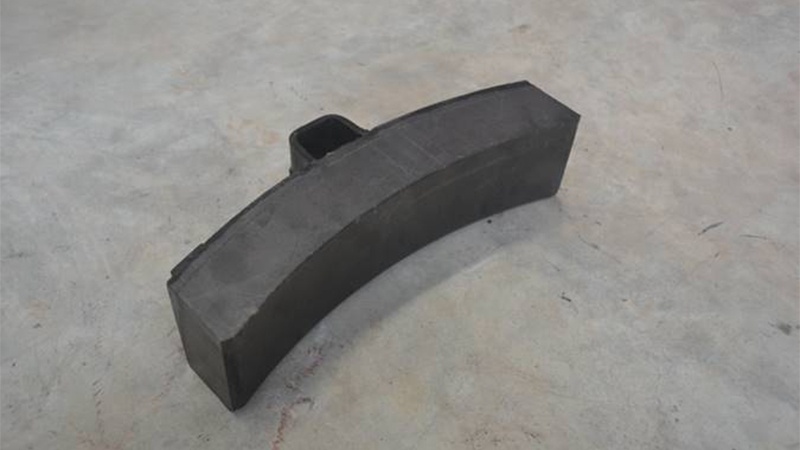
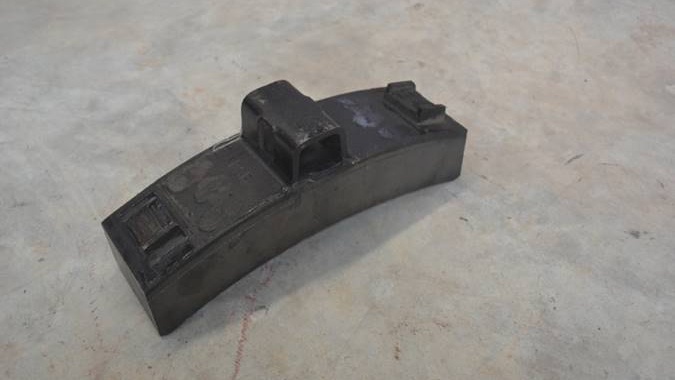
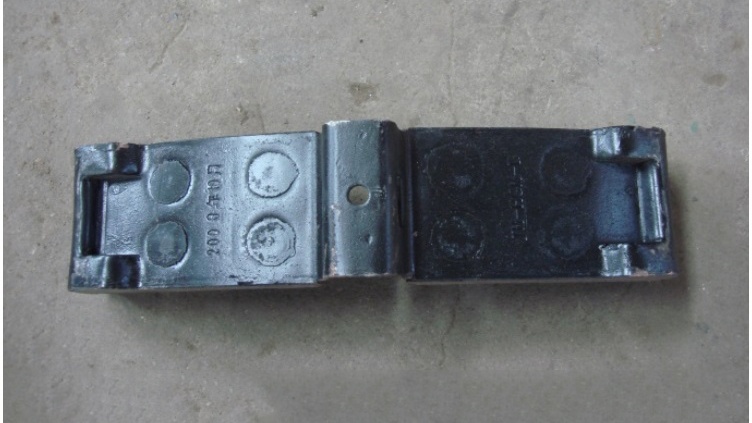
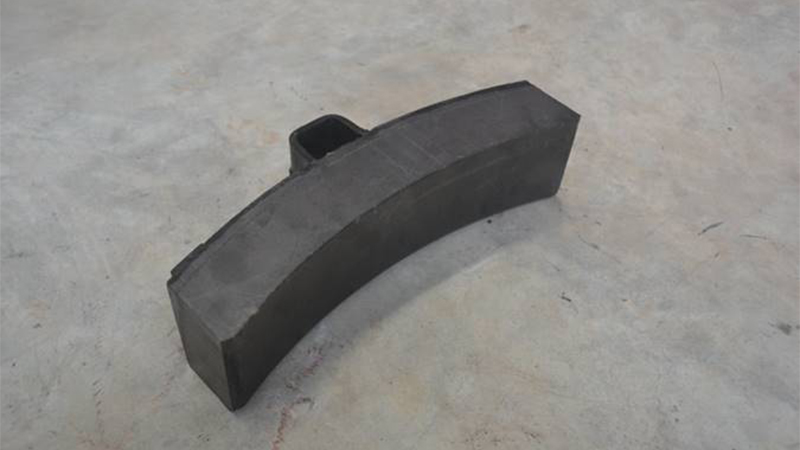
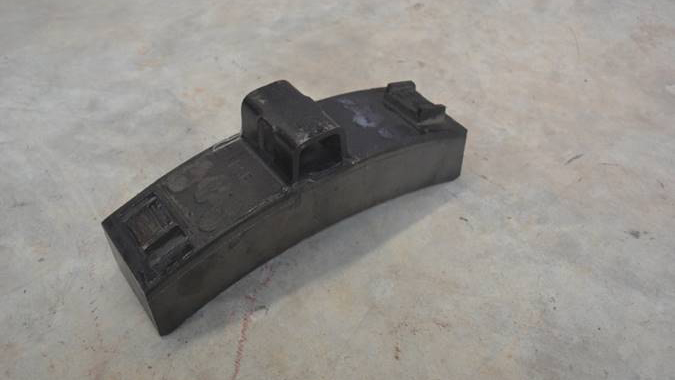
Railway AAR Standard Brake Pads Composite Material High Performanceh Performance
- Product No.:2023823204231
- Price:nogotiation
- Material:high-quality carbon steel
- Standard:AAR
- mould charge:yes
- Production time:60
- weight:17kgs
- Package:Wood Box
Product Description
Title: Railway AAR Standard Brake Pads – High Performance Composite Material for Reliable Locomotive Braking
Our Railway AAR Standard Brake Pads are engineered from high-performance composite material to deliver consistent, reliable braking for demanding locomotive and railcar applications. These pads represent a significant advancement over conventional brake shoes, utilizing a sophisticated organic non-asbestos composite formulation that combines exceptional friction characteristics with extended service life.
Manufactured to meet the stringent requirements of AAR M-926 – the only industry-wide specification for composition brake shoes in interchange freight and passenger service – our brake pads are designed to pass the comprehensive AAR dynamometer test regimen . This includes grade tests, light and heavy braking stop tests, static friction tests, and wear evaluations, ensuring performance that railroads trust .
Composite Material Composition:
Our brake pads utilize a proprietary composite friction element consisting of:
-
Rubber Binder Matrix: Vulcanizable natural and synthetic rubber compounds (butyl rubber, styrene-butadiene copolymer, nitrile rubber) that form a hard, durable matrix
-
Aramid Polymer Fibers: High-strength synthetic fibers that impart wear resistance and reinforce the composite structure
-
High Oil Absorption Fillers: Specialized fillers with oil absorption values of at least 30, crucial for achieving the required friction coefficient
-
Phenolic Resin Binders: Novalac-type phenolic resins that enhance thermal stability and structural integrity
-
Thermosetting Resin Additives: Phenol-aldehyde resins (1–10% by weight) that serve as strengthening agents
Key Performance Characteristics:
| Parameter | Specification |
|---|---|
| Average Coefficient of Friction | 0.27 – 0.45 μ (dry & wet conditions) |
| Minimum AAR Acceptance COF | 0.27 (heavy braking) / 0.32 (light braking) |
| Minimum Static COF | 0.38 |
| Density | 2.40 – 2.70 g/cm³ |
| Maximum Operating Temperature | 400°C (peak 500°C) |
| Classification | High Friction Composition (K-Type per UIC) |
Applications:
-
Locomotives (freight and passenger)
-
Freight wagons
-
Passenger coaches (including LHB coaches up to 200 km/h)
-
High-speed rail applications
Standards Compliance:
-
AAR M-926 (Brake Shoes – High Friction Composition Type)
-
UIC 541-4 (Composite Brake Blocks – General Certification Conditions)
-
TB/T 3196 (Composite Brake Shoes for Locomotives)
Technical Specifications
1. Material Composition
Component
Percentage (Approx.)
Function
Rubber Binder
Primary matrix
Structural bonding, impact absorption
Phenolic Resin
1 – 10% by weight
Strengthening, thermal stability
Aramid Polymer Fibers
Minor proportion
Wear resistance, reinforcement
Friction Modifiers
Up to 15% by volume
Coefficient of friction control
Mineral Fillers
Variable
Friction promotion, thermal management
Vulcanizing Catalysts
1 – 3% by weight
Rubber curing acceleration
| Component | Percentage (Approx.) | Function |
|---|---|---|
| Rubber Binder | Primary matrix | Structural bonding, impact absorption |
| Phenolic Resin | 1 – 10% by weight | Strengthening, thermal stability |
| Aramid Polymer Fibers | Minor proportion | Wear resistance, reinforcement |
| Friction Modifiers | Up to 15% by volume | Coefficient of friction control |
| Mineral Fillers | Variable | Friction promotion, thermal management |
| Vulcanizing Catalysts | 1 – 3% by weight | Rubber curing acceleration |
2. Manufacturing Process
Step
Description
1. Raw Material Blending
Precise weighing and mixing of rubber binders, aramid fibers, fillers, and resin components
2. Cold Molding
Rigid cold molding process to form the pad shape
3. Compression Molding
Injection or compression molding at controlled temperature and pressure
4. Thermal Curing
Vulcanization of rubber matrix and polymerization of phenolic resin
5. Post-Cure Processing
Controlled cooling and conditioning to achieve final properties
6. Quality Inspection
Dimensional check, hardness, density, and friction coefficient verification
| Step | Description |
|---|---|
| 1. Raw Material Blending | Precise weighing and mixing of rubber binders, aramid fibers, fillers, and resin components |
| 2. Cold Molding | Rigid cold molding process to form the pad shape |
| 3. Compression Molding | Injection or compression molding at controlled temperature and pressure |
| 4. Thermal Curing | Vulcanization of rubber matrix and polymerization of phenolic resin |
| 5. Post-Cure Processing | Controlled cooling and conditioning to achieve final properties |
| 6. Quality Inspection | Dimensional check, hardness, density, and friction coefficient verification |
3. Physical Properties
Property
Value
Density
2.40 – 2.70 g/cm³
Hardness (HRX)
24 – 45
Cross Breaking Strength
≥100 kg/cm²
Shear Strength
≥8.0 KN
Compression Modulus
1000 – 3000 N/mm²
Acetone Extract
≤3.0%
Loss on Ignition
≤15%
| Property | Value |
|---|---|
| Density | 2.40 – 2.70 g/cm³ |
| Hardness (HRX) | 24 – 45 |
| Cross Breaking Strength | ≥100 kg/cm² |
| Shear Strength | ≥8.0 KN |
| Compression Modulus | 1000 – 3000 N/mm² |
| Acetone Extract | ≤3.0% |
| Loss on Ignition | ≤15% |
4. Friction Performance
Parameter
Specification
Classification
High Friction Composition (H-Type)
Average COF (Dry)
0.35 – 0.45 μ
Average COF (Wet)
0.27 – 0.35 μ
AAR Light Braking COF
≥0.32
AAR Heavy Braking COF
≥0.27
Static COF
≥0.38
| Parameter | Specification |
|---|---|
| Classification | High Friction Composition (H-Type) |
| Average COF (Dry) | 0.35 – 0.45 μ |
| Average COF (Wet) | 0.27 – 0.35 μ |
| AAR Light Braking COF | ≥0.32 |
| AAR Heavy Braking COF | ≥0.27 |
| Static COF | ≥0.38 |
5. Operating Specifications
Parameter
Specification
Maximum Operating Temperature
400°C
Peak Temperature
500°C
Maximum Brake Force on Disc
5.0 Tons
Suitable Speed Range
Up to 200 km/h
| Parameter | Specification |
|---|---|
| Maximum Operating Temperature | 400°C |
| Peak Temperature | 500°C |
| Maximum Brake Force on Disc | 5.0 Tons |
| Suitable Speed Range | Up to 200 km/h |
Maintenance Guidelines
Proper maintenance of AAR standard composite brake pads is essential for ensuring safe and reliable braking performance. Follow these guidelines to maximize service life and maintain operational safety .
1. Periodic Inspection
Inspection Frequency: Conduct visual inspections at regularly scheduled maintenance intervals per APTA RT-VIM-S-007-02 guidelines .
Visual Inspection Checklist:
-
Check brake pad wear: new pad thickness is 35 mm, minimum allowable thickness is 7 mm
-
Inspect for cracks, damage, or missing components
-
Look for foreign objects embedded in the friction surface
-
Check for oil or grease contamination on pad surface
-
Inspect pad holders for play and proper seating
-
Check for presence of dust or greasy material on calipers and actuators
2. Wear Monitoring
Wear Limit Indicators:
-
Brake pads should incorporate wear indicators or matchmarks to determine the minimum permissible thickness for replacement
-
Replace pads when thickness reaches 7 mm minimum
-
If one pad is worn out, replace in full set formation (all pads on the axle)
Monitoring Notes:
-
Monitor play of brake pads in holders
-
Visual check should include both pad surface and backing plate condition
-
Document wear measurements at each inspection interval
3. Cleaning and Contamination Control
Recommended Practices:
-
Remove dust and greasy material sticking to brake calipers and actuators with suitable tools
-
Ensure no lubricant drops on brake discs
-
Keep friction surfaces clean and free from contaminants
-
Do not use solvents that may degrade the composite material
Precautions:
-
Avoid contact with petroleum-based solvents
-
Do not attempt to clean pads by sanding or grinding – replace if contaminated
-
Store pads in clean, dry environment away from oil and grease
4. Replacement Procedures
When to Replace:
-
Wear limit reached (7 mm minimum thickness)
-
Cracks or visible damage detected
-
Contamination that cannot be removed
-
Uneven wear patterns indicating misalignment
Replacement Guidelines:
-
Always replace pads in full sets per axle
-
Clean pad holders and calipers before installing new pads
-
Ensure proper seating of new pads in holders
-
Check pad play after installation
-
Perform brake function test after replacement
5. Storage and Handling
Storage Condition
Requirement
Temperature
Ambient (0°C – 40°C)
Humidity
Dry environment, avoid moisture
Contamination Prevention
Protect from oil, grease, and solvents
Shelf Life
Consult manufacturer's recommendation
Stacking
Do not stack excessively; store on clean, flat surfaces
| Storage Condition | Requirement |
|---|---|
| Temperature | Ambient (0°C – 40°C) |
| Humidity | Dry environment, avoid moisture |
| Contamination Prevention | Protect from oil, grease, and solvents |
| Shelf Life | Consult manufacturer's recommendation |
| Stacking | Do not stack excessively; store on clean, flat surfaces |
6. Safety Precautions
-
Always follow established lock-out/tag-out procedures when working on brake systems
-
Wear appropriate PPE (gloves, eye protection)
-
Do not inhale dust from worn brake pads
-
Dispose of used pads in accordance with local environmental regulations
Always follow established lock-out/tag-out procedures when working on brake systems
Wear appropriate PPE (gloves, eye protection)
Do not inhale dust from worn brake pads
Dispose of used pads in accordance with local environmental regulations
Related Products
Price: nogotiation
Price: nogotiation
Price: nogotiation
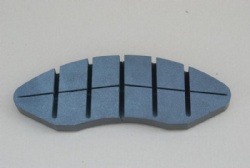
Price: nogotiation
Price: nogotiation
Products Category
Contact Us
Name: Meiya
Tel: +86 15151598778
E-mail: meiya@guarail.com
WeChat: +86 15151598778
Whatsapp: +86 15151598778
Add: B1608 room Building 5 of Tainhe Huayuan ,YangJian Twon,Suzhou city ,Jiangsu ,China

 WhatsApp
 Mail inquiry