
Products >> Railway Track and Fastern >>
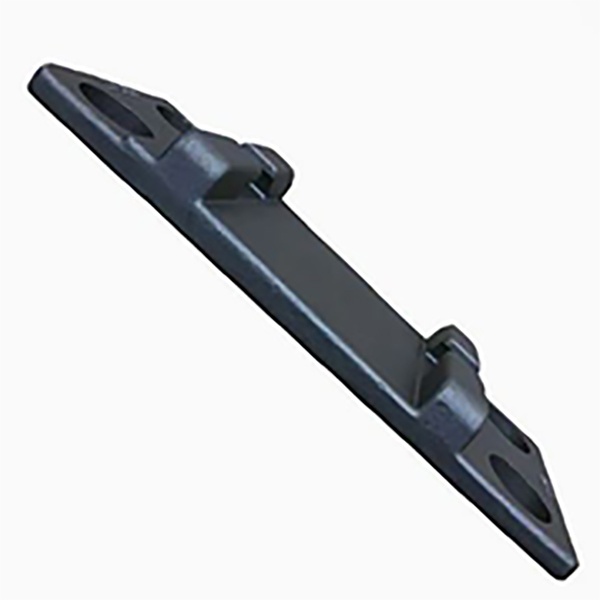
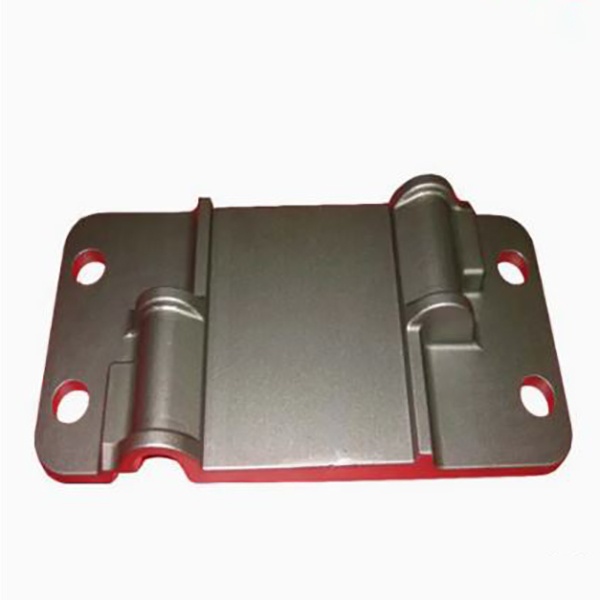

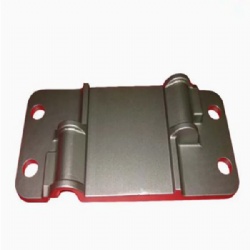
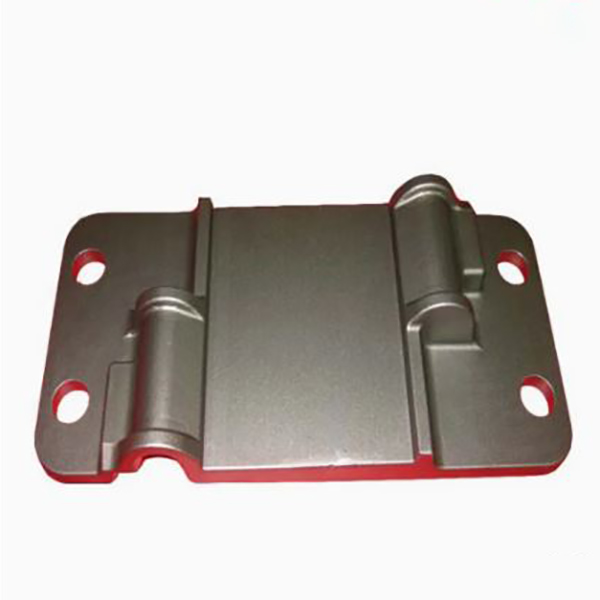
Railway casting steel rail tie plate of rail fasten parts
- Product No.:2026728104217
- Price:nogotiation
- Material:high-quality carbon steel
- Standard:AAR or GB
- mould charge:yes
- Production time:60
- weight:30
- Package:Wooden Box
1. Product Overview
The railway casting steel rail tie plate (also known as base plate or sole plate) is a critical load‑bearing component in railway fastening systems. Installed between the rail foot and the sleeper (timber or concrete), it performs the following essential functions:
-
Load Bearing and Transmission – It receives the train loads from the rail and distributes them evenly over the sleeper and ballast bed, preventing localised stress concentrations that could damage the sleeper.
-
Gauge Retention – The integral shoulders on the tie plate restrain lateral displacement of the rail, ensuring that the track gauge (e.g., standard gauge 1435 mm) remains within design limits.
-
Providing Rail Cant – The bearing surface is machined with a specific slope (typically 1:40) to induce an inward cant (rail inclination), optimising wheel‑rail contact geometry.
-
Extending Sleeper Life – By increasing the contact area between the rail base and the sleeper, it significantly reduces wear on the sleeper surface.
Manufactured by cast steel processes, this product offers superior strength, toughness and impact resistance compared to cast iron plates, making it particularly suitable for heavy‑haul railways, high‑speed lines and high‑axle‑load freight routes.
2. Product Classification
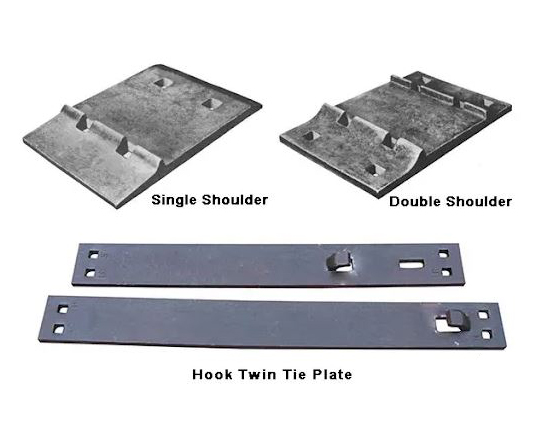
Based on shoulder configuration, cast steel tie plates are mainly classified as follows:
| Type | Characteristics | Application |
|---|---|---|
| Single‑Shoulder Plate | Shoulder only on the field side; no shoulder on the gauge side | Light‑duty lines, rail weights 56 lb ~ 100 lb |
| Double‑Shoulder Plate | Shoulders on both sides of the rail – stronger rail restraint | Heavy‑haul & high‑speed lines, rail weights >100 lb |
| No‑Shoulder Plate | Without shoulders | Specific fastening systems |
The double‑shoulder type is currently the most widely used worldwide. According to the number of bolt holes, they are also available in 2‑hole, 4‑hole, 5‑hole, 6‑hole and 8‑hole configurations.
3. Technical Parameters
3.1 Common Specifications
Below are typical dimensions for cast steel tie plates (custom sizes available on request):
| Model | Dimensions (mm) | Hole Dia. (mm) | No. of Holes | Rail Cant | Rail Type | Weight (kg) |
|---|---|---|---|---|---|---|
| Rph 1/160 | 345/285/127/160×15/13 | Ø 26 | 4 | 1:40 | S49/S54 | 7.86 |
| Rp 01/01/160 | 345/285/127/160×15/13 | Ø 26 | 4 | 1:40 | S49/S54 | 7.70 |
| Rph 1/210 | 345/285/127×210×15/13 | Ø 26 | 4 | 1:40 | S49/S54 | 10.55 |
| Rph 1/210 | 345/285/127×210×15/13 | Ø 36.3 | 2 | 1:40 | S49/S54 | 10.55 |
| Rph 1/210 FVZ | 345/285/127×210×15/13 | Ø 26 | 4 | 1:40 | S49/S54 | 10.69 |
| Sph 1(a) | 345/350/127×410×15/13 | Ø 26 | 8 | 1:40 | UIC60 | 20.60 |
| Rph 6/160 | 370/310/152×160×15/13 | Ø 26 | 4 | 1:40 | UIC60 | 8.44 |
| Rph 6/210 | 370/310/152×210×15/13 | Ø 26 | 4 | 1:40 | UIC60 | 11.32 |
| SZ 60 | 370/350/152×420×15/13 | Ø 26 | 8 | 1:40 | UIC60 | 22.73 |
| Rph 11 Ü | 664/554×160 | Ø 26 | 4 | 1:40 | S54 | 15.37 |
| Rph 13 Ü | 690/570×160 | Ø 26 | 4 | 1:40 | UIC60 | 15.27 |
| Rpo 5 | 345/285/127×160×15/13 | Ø 26 | 4 | 1:20 | S49/S54 | 8.00 |
Note: Dimension notation (e.g., 345/285/127/160×15/13) indicates length/width/thickness/other dimension × plate thickness/shoulder height – please refer to customer drawings for exact interpretation. All specifications can be custom‑made according to client drawings or samples.
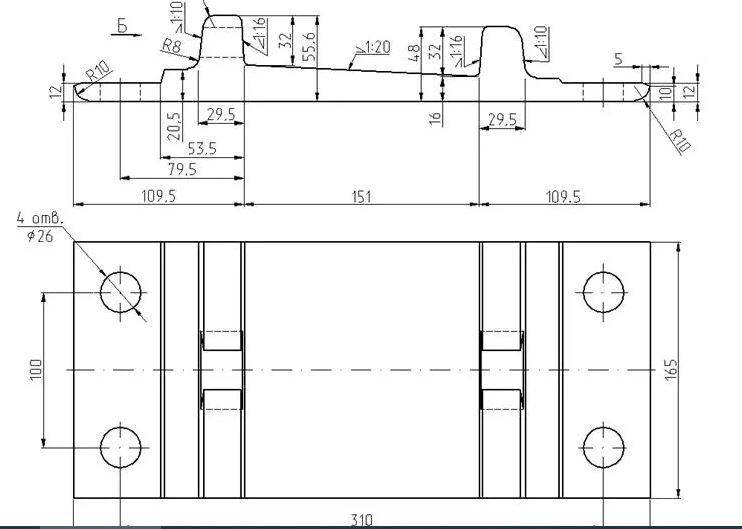
3.2 Dimensional Tolerances
In accordance with general industry practice:
| Parameter | Tolerance (mm) |
|---|---|
| Thickness | ±1.0 |
| Width | ±3.0 |
| Length | ±4.0 |
| Edge distance of holes | ±0.5 |
| Hole spacing | ±1.0 |
4. Material & Chemical Composition
4.1 Common Material Grades
The following grades are available depending on service conditions:
-
Cast steel: ZG230‑450, ZG270‑500, ZG25, ZG35, ZG45
-
Ductile iron: QT450‑10, QT500‑7, QT600‑3
-
Carbon steel: Q235, 20#, 35#, 45#
-
Low‑alloy cast steel: ZG25MnCrNiMo, etc.
4.2 Typical Chemical Composition (QT500‑7)
| Element | Content (%) |
|---|---|
| C | 3.60 ~ 3.80 |
| Mn | ≤ 0.6 |
| Si | 2.50 ~ 2.90 |
| P | ≤ 0.08 |
| S | ≤ 0.025 |
(For QT450‑10: C 3.40‑3.90, Mn 0.2‑0.5, Si 2.70‑3.00, P≤0.07, S≤0.03)
4.3 Mechanical Properties
| Grade | Tensile Strength (MPa) | Hardness (HB) | Elongation (%) |
|---|---|---|---|
| QT450‑10 | ≥450 | 170‑230 | ≥10 |
| QT500‑7 | ≥500 | — | ≥7 |
| ZG230‑450 | ≥450 | — | ≥5 |
| ZG270‑500 | ≥500 | — | ≥5 |
5. Applicable Standards
Our products are manufactured and inspected in accordance with the following international, national and industrial standards:
| Standard Code | Title / Scope |
|---|---|
| AREMA Chapter 5 Part 1 | American Railway Engineering and Maintenance‑of‑Way Association – Rail Tie Plates |
| ASTM A67 | Standard Specification for Steel Tie Plates (Grade 1 Low‑Carbon / Grade 2 High‑Carbon) |
| UIC 864‑6 | International Union of Railways – Tie Plate Standard |
| GB/T 1348 | Ductile Iron Castings (China) |
| TB/T 3395 | Castings for High‑Speed Railway Fastening Systems (China) |
| DIN EN 1561 | Cast Iron with Lamellar Graphite (Germany/Europe) |
| EN 13481 | Railway Applications – Track – Fastening Systems (Europe) |
Custom non‑standard sizes can also be produced according to customer drawings or samples.
6. Manufacturing Process
6.1 Casting Process
Cast steel tie plates are mainly produced via:
-
Sand Casting – Economical for high‑volume production.
-
Lost Foam Casting – High precision and good surface finish, suitable for complex shapes.
-
Investment Casting – Excellent dimensional accuracy for demanding applications.
Process flow: Tooling design → Moulding/core‑making → Melting (medium‑frequency induction furnace, pouring temperature ~1580°C) → Pouring (vacuum maintained at 0.03 MPa) → Cooling → Shakeout & cleaning → Heat treatment (if required) → Surface finishing.
6.2 Alternative Processes (Optional)
Besides casting, tie plates can also be manufactured by forging or rolling. Forged plates have simpler geometry and lower tooling costs; cast plates allow more complex shapes (especially double‑shoulder designs). The optimal process can be selected based on specific requirements.
7. Surface Treatment
To enhance corrosion resistance and service life, we offer the following surface finish options:
| Treatment | Features |
|---|---|
| Plain (as‑cast) | No additional coating, suitable for general environments |
| Oil Coating | Rust‑preventive oil for short‑term protection |
| Sandblasting | Removes scale and improves paint adhesion |
| Painting / Electrostatic Powder Coating | Long‑term anti‑corrosion for harsh environments |
| Black Oxide (Oxidising) | Decorative black finish with moderate corrosion protection |
Related Products

Price: nogotiation

Price: nogotiation

Price: nogotiation

Price: nogotiation

Price: nogotiation

Price: nogotiation
Products Category
Contact Us
Name: Meiya
Tel: +86 13862216492
E-mail: meiya@guarail.com
WeChat: +86 13862216492
Whatsapp: +86 13862216492
Add: B1608 room Building 5 of Tainhe Huayuan ,YangJian Twon,Suzhou city ,Jiangsu ,China

 WhatsApp
 Mail inquiry

